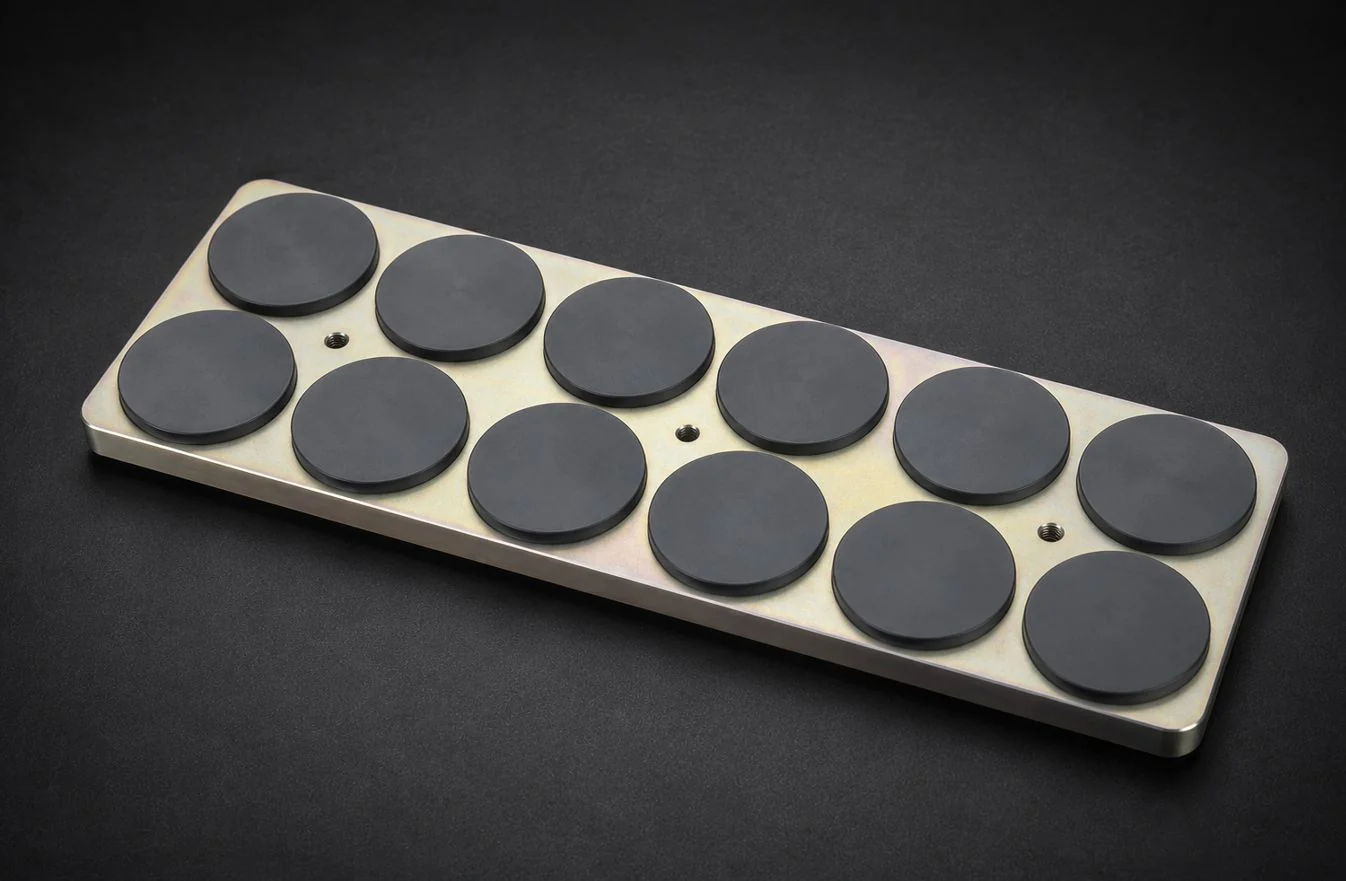
Custom wind turbine brake pads for yaw and rotor brakes
FTL is a custom wind turbine brake pad manufacturer, making new, existing and obsolete yaw and rotor brake pads for wind programmes in the UK and Europe.
Start with the application, an existing pad, a drawing or the performance problem, not simply a part number.
We develop the friction material and the complete pad around what the yaw or rotor brake must do, the conditions it runs in and the evidence required before repeat supply.
For the wider sector context, explore our wind energy materials and engineering.
When wind teams need a custom brake pad
The correct route depends on what has prompted the requirement.
A new turbine or brake programme needs a custom pad
The yaw or rotor braking function is understood, but the friction material, pad construction or repeatable production route has not yet been established. FTL can support the programme from application review and material selection through prototypes, testing, validation support and controlled repeat manufacture.
New Programme Support →An existing yaw or rotor brake pad is not performing as required
Inconsistent braking, excessive or unpredictable wear, thermal-performance concerns, or variation between manufactured pads or production batches. FTL can review the available evidence across the friction material, complete pad, operating environment and production route.
Performance Optimisation →An original pad, material or supplier is no longer available
The turbine must stay in service, but the original material, drawing, supplier or complete brake pad has become obsolete. FTL can review the existing pad and available evidence before proposing a redevelopment, prototype and revalidation route.
Legacy & Obsolete Reverse Engineering →The pad currently passes through too many suppliers
The friction material, backing plate, machining, bonding, finishing and inspection are divided between separate organisations. FTL can connect the relevant stages through one accountable manufacturing route.
Single-Source Friction Manufacturing →A prototype must progress into controlled repeat supply
The engineering solution needs to move into a defined production arrangement supported by repeat manufacturing controls, inspection, traceability, inventory holding, scheduled call-off, customer-specific packaging and identification, and delivery.
New Programme Support
For a new yaw or rotor brake requirement that needs a defined friction-material, pad-construction and manufacturing route. Support can include application review, material selection or formulation, pad and backing-plate engineering, prototype manufacture, testing and inspection, validation support and transfer into controlled repeat production.
Legacy & Obsolete Component Reverse Engineering
For a wind turbine pad still required after its original material, drawing, supplier or finished component becomes unavailable. Support can include existing-pad and evidence review, dimensional assessment, geometry redevelopment, alternative material selection or development, prototype manufacture, testing and revalidation support and repeat manufacture.
Friction System Performance Optimisation
For an existing yaw or rotor brake pad with inconsistent braking, excessive or unpredictable wear, thermal-performance concerns or production-repeatability problems. Support can include symptom and evidence review, operating-condition assessment, investigation of material and component factors, alternative formulation or component work, comparative prototypes, testing and inspection and implementation support.
Move from a brake-pad requirement to a controlled engineering and supply route
A custom wind turbine brake-pad project should define more than the pad's visible shape.
The engineering route must establish the required function, friction material, complete-pad construction, manufacturing stages, inspection evidence and responsibilities that apply before repeat supply begins.
Potential engineering outcomes
- A shared definition of the application and required braking or holding function
- A friction-material selection or development route
- A defined pad geometry and backing-plate route
- A prototype and test plan
- Agreed inspection and acceptance requirements
- Clear FTL and customer validation responsibilities
- A documented decision on whether further development is required
Potential manufacturing and supply outcomes
- One accountable route from friction material to finished pad
- Controlled machining, bonding, finishing and inspection
- Defined production records and traceability
- Progression from prototype into repeat manufacture
- Inventory and scheduled call-off where agreed
- Customer-specific packaging and labelling
- Scheduled delivery
Performance, service life, lead time and approval outcomes depend on the application, available information, agreed testing and respective customer and FTL responsibilities.
What a wind turbine brake-pad project can include
Not every project requires every stage. FTL can make the friction material, the finished pad or the complete brake component.
For FTL's composite yaw pads, backing plates are available in steel or in glass-fibre reinforced material, and the pads are made to a tight tolerance so they sit in the brake calliper without lateral movement. A complete project can draw on friction-material selection, pad and backing-plate engineering, machining, bonding, surface preparation, finishing, assembly, inspection and the move into controlled repeat supply.
Small batches, prototypes and repeat supply
FTL makes wind turbine brake pads in small batches as well as in repeat production.
A project can start with prototype pads, move to a low-volume batch and then into scheduled production, with finished pads held for call-off where agreed. FTL's minimum order depends on the part and the enquiry, and is confirmed for each component with the quantity range, set-up and commercial fit. For a pad that is no longer made, the reverse engineering route starts from the existing part.
What FTL needs to understand before recommending a brake-pad route
A material name, nominal coefficient or existing part number does not define the complete requirement.
Begin with the brake and what the pad must achieve.
What is the application?
- Yaw brake, or rotor or other disc brake
- What the brake is required to stop or hold
- Whether the turbine is new or already in service
- What has prompted the enquiry
- Whether the requirement is for a material, finished pad or complete bonded component
Is this a new design or an existing brake pad?
- A new programme
- A new pad for an existing turbine
- An existing pad under performance review
- An obsolete pad
- A supply-continuity issue
- A prototype moving towards production
What conditions will the pad run in?
- Applied load or pressure
- Relative speed
- Temperature
- Contamination
- Braking or holding duration
- Operating frequency
- Environmental exposure
- Known wear or thermal concerns
A yaw-brake set: the friction pads, in green, clamping the yaw ring. Every question reads into the same component.
What technical information is available?
- The existing pad
- Drawings or partial drawings
- Component dimensions
- Backing-plate information
- Number and arrangement of pads
- Mating-surface information
- Required performance
- Test or inspection records
A complete technical pack is not required before the first conversation.
What must the finished pad demonstrate?
- Required friction behaviour
- Wear expectations
- Thermal requirements
- Dimensional requirements
- Bonding or backing-plate requirements
- Inspection requirements
- Acceptance evidence
- Validation and approval responsibilities
How will the pads be manufactured and supplied?
- Prototype quantities
- Expected annual volumes
- Repeat-production schedules
- Inspection frequency
- Inventory holding
- Scheduled call-off
- Packaging, labelling and identification
- Delivery requirements
Expected annual volumes are discussed after the application and technical fit have been established.
Select the friction material around the complete wind turbine brake
Composite and organic grades for yaw brakes, organic and sintered grades for rotor and other disc brakes. Every grade opens its technical data sheet.
| Grade | Type | Material | Used for | Running condition | Friction co, dynamic / static |
|---|---|---|---|---|---|
| FTL-207 | Composite | Carbon composite on an optional glass-fibre reinforced supporting layer | Wind turbine yaw systems | On request | 0.30 to 0.40 |
| FTL201 | Composite | Medium-coefficient plastic composite on a glass-fibre reinforced layer | Wind turbine yaw brakes | Oil, chemical and grease resistant | 0.32 / 0.48 |
| FTL203 | Composite | Low-coefficient plastic composite on a glass-fibre reinforced layer | Wind turbine yaw brakes | Oil, chemical and grease resistant | On request / 0.15 |
| FTL204 | Composite | Low-coefficient plastic composite on a glass-fibre reinforced layer | Wind turbine yaw brakes | Oil, chemical and grease resistant | 0.25 / 0.35 |
| FTL087 | Organic | Rigid moulded, medium-high friction coefficient | Wind turbine yaw brakes | Oil resistant | 0.45 / 0.50 |
| FTL135.2DNV-GL approved | Organic | Rigid moulded, resin based, non-asbestos mineral fibres | Disc brake pads for wind turbines | On request | 0.40 / 0.45 |
| FTL004 | Sintered | Copper-based sintered | Wind energy brake pads | Dry | 0.48 / 0.50 |
| FTL509 | Sintered | Metal-ceramic, bronze-graphite, joined to a steel back plate | Wind energy brake pads | Dry | 0.45 / 0.55 |
| FTL510 | Sintered | Copper-based sintered, free of asbestos, lead and zinc | Wind turbines | Dry; not for oil | 0.42 / 0.50 |
| FTL511 | Sintered | Moulded sinter metal on an iron, bronze, hard metal and ceramic basis | Wind generators | Oil resistant | 0.42 / 0.50 |
| FTL513 | Sintered | Copper-based sintered for high-energy systems, no asbestos, lead or zinc | Wind turbines | On request | 0.40 / 0.50 |
NOTE Summary values are indicative and must be read with the full data sheet and its stated test conditions. FTL-207 carries one friction range rather than a dynamic and static pair; its full specification is on the FTL-207 material specification.
Inputs that shape the material decision
- Required braking or holding behaviour
- Coefficient stability
- Wear rate
- Thermal performance
- Load, speed, temperature, contamination
- Pad and backing-plate geometry
- Bonding and finishing requirements
- Inspection and validation evidence
Published data is a starting point. Final material selection depends on the complete application and agreed validation route.
A controlled path from brake-pad brief to repeat manufacture
The exact sequence varies by project, but each stage should produce enough evidence to support the next engineering decision.
Establish technical fit
- Application + required function
- New, existing or obsolete
- Programme stage
- Performance or supply concern
- Information available
Define application requirements
- Yaw or rotor brake
- Load, speed, temperature, contamination
- Pad, backing-plate and calliper information
- Required braking behaviour
- Existing performance evidence
- Inspection and documentation needs
Establish material and component route
- Established grade or development work
- Pad geometry development
- Backing plate
- Machining, bonding, finishing, inspection stages
- What remains unknown
Agree prototype and test plan
- Material or component variants
- Prototype quantities
- Manufacturing stages
- Features and dimensions to inspect
- Tests + acceptance evidence
- FTL and customer responsibilities
Manufacture the prototype pads
- Friction-material production
- Friction and metallic-component machining
- Surface preparation
- Bonding, finishing, assembly
- Inspection
Test, inspect and refine
- Agreed material, dynamic, dimensional or bond testing
- Evidence reviewed against requirements
- Revise material, geometry or route where needed
Support validation and approval
- Engineering, manufacturing, test, inspection and traceability evidence within scope
- Final turbine, system, customer or regulatory approval responsibilities agreed per project
Transfer into controlled repeat supply
- Repeat-production controls
- Inspection and traceability
- Inventory holding, scheduled call-off
- Customer-specific packaging and identification
- Export documentation and delivery
Testing and inspection tied to defined engineering questions
Testing should be selected around what the project needs to establish, not used as a general claim that a pad will perform in every wind turbine brake.
Depending on the agreed scope, a project can draw on coefficient-stability and wear-rate assessment, thermal-performance and bond-integrity testing, CMM dimensional inspection and production evidence such as in-process checks, final inspection and batch traceability. The available methods, conditions and acceptance evidence are described in full on the testing and inspection capability page.
The exact samples, test conditions, methods, acceptance criteria and customer responsibilities must be agreed before testing begins.
Keep the friction material connected to the finished brake pad
A fragmented route can divide responsibility between the material formulator, friction-component machinist, backing-plate supplier, bonder, finisher, test provider and inspector.
FTL can connect the relevant stages through one engineering and manufacturing chain, helping keep the material, component and production decisions aligned and the friction material connected to the finished pad.
The full connected route, from application review through friction-material selection, machining, bonding, finishing, testing and traceability to scheduled supply, is set out on the Single-Source Friction Manufacturing page.
Actual lead-time, procurement or cost benefits depend on the current supply arrangement and agreed project scope.
Wind turbine brake pads for yaw and rotor brakes
FTL's wind grades cover yaw brakes, rotor and other disc brakes, and wider turbine and generator braking.
Each enquiry still requires review of the individual turbine, brake and operating environment.
Yaw brakes
Composite yaw pad materials FTL-207, FTL201, FTL203 and FTL204, with FTL-207 formulated and optimised for wind turbine yaw systems, and the organic grade FTL087. Wear in a yaw brake depends on braking force, sliding speed and distance, how often the system moves and the mating surface, so the pad is chosen around the installation.
Rotor and other disc brakes
FTL135.2, a DNV-GL approved organic material, for disc brake pads on wind turbines, and the sintered grades FTL004 and FTL509 for wind energy brake pads, both made for dry running. FTL509 is joined to a steel back plate.
Wider turbine and generator braking
The sintered grades FTL510 and FTL513 for wind turbines and FTL511 for wind generators. FTL510 and FTL513 are free of asbestos, lead and zinc; FTL511 is oil resistant.
Oil, grease and chemical exposure
FTL201, FTL203 and FTL204 suit installations where oil contamination is likely, and resist chemicals and grease. FTL087 and FTL511 are also oil resistant.
These are application contexts rather than stock product categories. FTL should confirm technical fit for every enquiry.
Questions buyers need answered before approving a wind turbine brake pad
Can FTL match or improve the current material performance?
FTL can review the current pad, available material information, operating conditions and required behaviour before proposing an established, optimised or newly developed route. Whether performance can be matched or improved depends on available application evidence, defined operating conditions, complete pad construction, agreed test conditions, acceptance criteria and validation responsibilities. No outcome is promised before the review and required development work are complete.
Is the proposed pad already proven in service?
Where relevant application history or established-material evidence exists, FTL can identify it during the technical discussion. A new, modified or redeveloped wind application may still require project-specific testing and customer validation.
How does FTL support consistent quality and repeatability?
The available route connects friction-material formulation, pad and backing-plate engineering, machining, surface preparation, bonding, finishing, testing, inspection, production documentation and batch and lot traceability. The exact production controls and acceptance requirements are agreed for the individual project.
Can FTL manufacture the complete pad?
Yes, where the project fits FTL's confirmed scope. FTL can support the friction material and complete-pad route through engineering, machining, bonding, finishing, testing, inspection and repeat supply.
Can FTL supply the pads sooner?
There is no standard lead time for every wind turbine brake-pad project. Timing depends on information available, material-development work, pad and backing-plate complexity, prototype iterations, testing and inspection, customer validation, production quantities and supply requirements. FTL confirms the proposed stages and timing after the initial technical review.
Can the price be improved?
Pricing depends on the agreed engineering, material, component, testing, documentation, volume and supply scope. The first conversation establishes technical fit. Commercial options can then be reviewed against the actual requirement rather than a standard online price.
A trusted, accountable supplier since 2003
High-performance friction and braking solutions, backed by decades of in-house expertise and made in North Wales.
Company-level standards support organisational and manufacturing assurance. Material suitability, component acceptance and programme requirements must still be agreed for the individual wind application.
Brake-pad engineering backed by controlled manufacture
SDTS approached FTL after an original aircraft brake pad became unavailable. FTL redesigned the pad, established a replacement material route and manufactured a component aligned with the stated aeronautical technical requirements, supporting SDTS's modification-certification process. This is an aircraft brake-pad example that shows the manufacturing capability behind a redeveloped pad, rather than wind proof.
“To continue flying our aircraft, we approached FTL to find replacement solutions for our brake pad problem, as the original part was no longer available on the market. The quality of our discussions, from both a technical and commercial standpoint, FTL's responsiveness in redesigning the pad with a material that meets aeronautical technical requirements, and their ability to adapt to our aeronautical environment allowed us to certify a modification applicable to our aircraft. The quality of the manufactured product is remarkable. Thanks to FTL, we can continue to fly, land, and brake safely.”
Olivier Moulin 
Confirmed organisational proof
- More than 20 years of experience
- Friction and metallic-component machining
- Controlled bonding and finishing
- Material, dynamic and shear testing
- CMM dimensional inspection
- Batch and lot traceability
Is FTL the right route for your wind turbine brake-pad requirement?
FTL is a strong fit when:
- Your team has an application brief rather than a stock-parts request
- A new yaw or rotor brake pad requires a custom material or component route
- An existing pad has braking, wear or thermal concerns
- The original material, drawing, supplier or complete pad is obsolete
- The requirement includes a bonded pad or backing plate
- Prototype work may need to progress into repeat manufacture
- Testing, inspection and traceability matter
- You want fewer suppliers across material, machining, bonding and finishing
- The finished pads require scheduled supply
A different route may be more appropriate when:
- You need an off-the-shelf pad immediately
- You are purchasing solely by part number
- You need a stock catalogue
- Price is the only selection criterion
- No technical or manufacturing review is required
Frequently asked questions about wind turbine brake pads
Do wind turbines have brakes?
What is the difference between a yaw brake and a rotor brake?
What are wind turbine brake pads made of?
How often do yaw brake pads need replacing?
Where can a UK operator get wind turbine brake pads made?
Can FTL make brake pads for an older turbine whose original pads are no longer available?
Does FTL sell wind turbine brake pads by part number?
Can FTL supply the backing plate as well as the friction material?
Can FTL manufacture wind turbine brake pads to a drawing?
Can FTL work without the original drawing?
What testing and inspection can FTL support?
Can prototype pads progress into repeat production?
How quickly can FTL make wind turbine brake pads?
When are price and annual volumes discussed?
Ask an FTL engineer about wind turbine brake pads
A part number, a machine, or the problem in your own words.
Bring us the existing pad, drawing or performance problem.
Tell FTL what the brake pad needs to do, what has prompted the enquiry and what information your team currently has.
A short initial brief is enough.
The relevant technical, engineering and commercial team members can then review the operating conditions, material route, complete-pad requirements and most appropriate next step.
Optional drawing or specification upload available.